Company Introduction
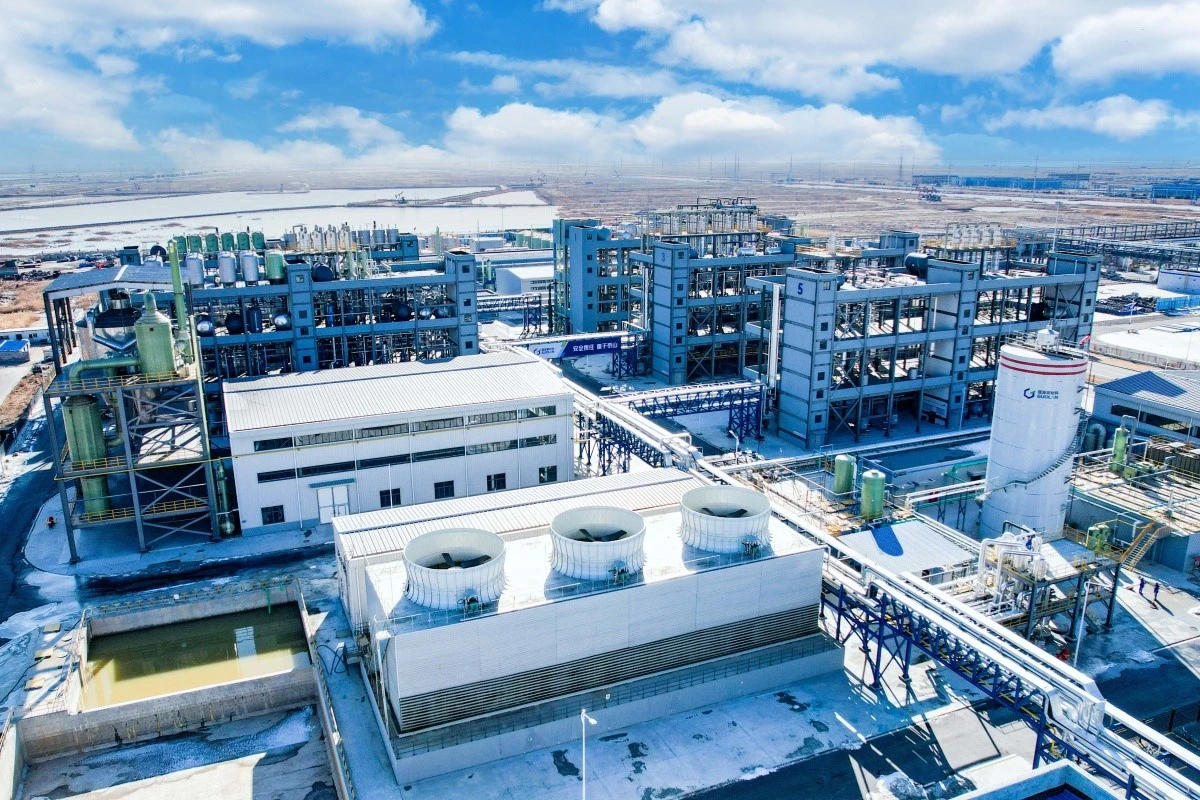
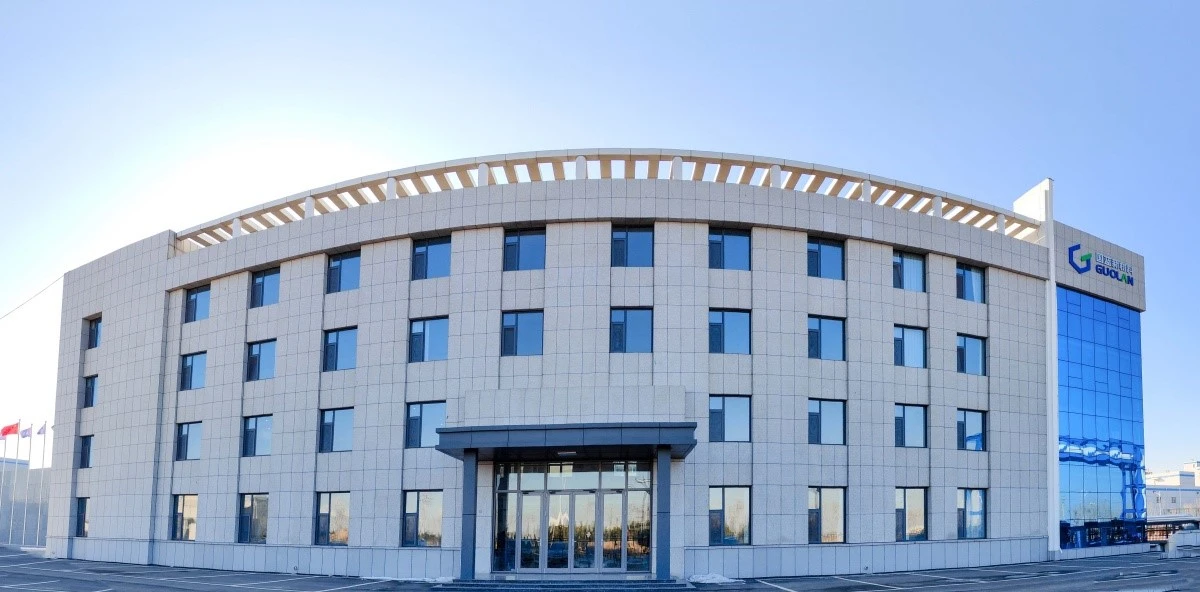
Guolan New Materials (Shandong) Co., Ltd. was established in November 2021 and is located in Dongying Port Economic Development Zone, Dongying City, Shandong Province, China. We are a professional manufacturer of organophosphorus products, integrating R&D, production, and sales.
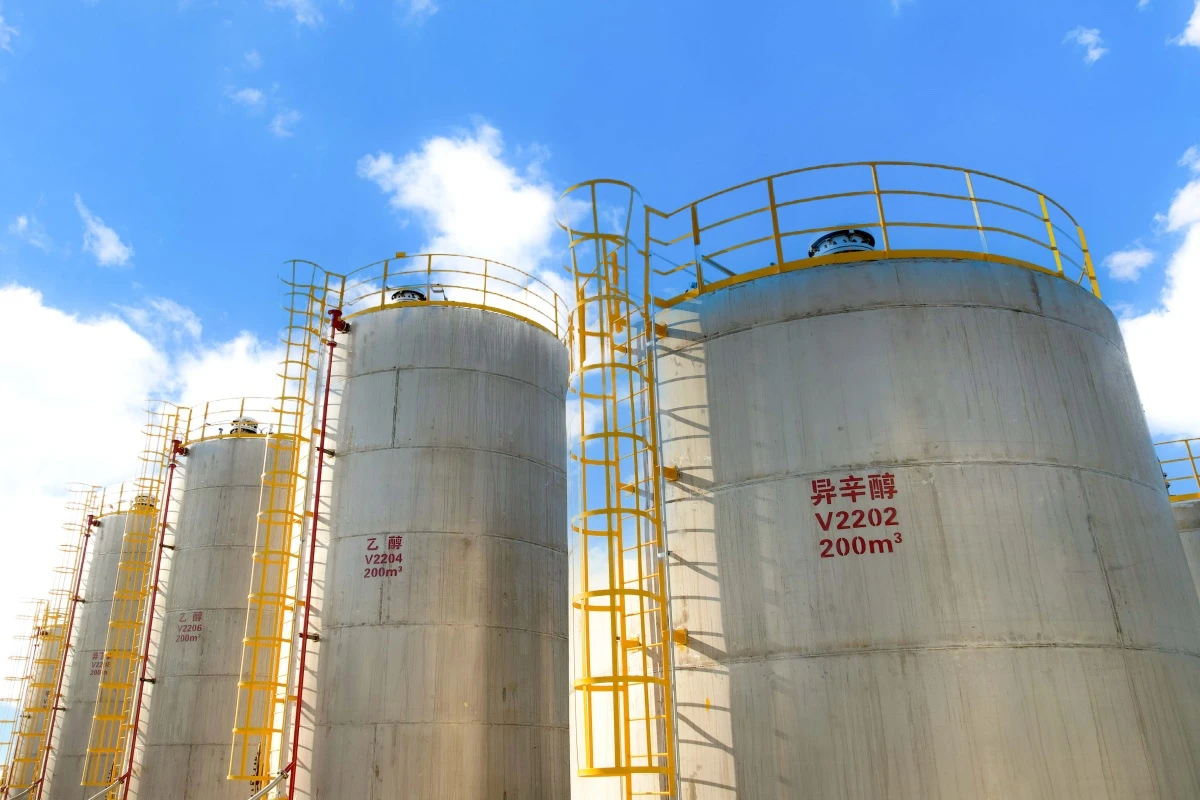
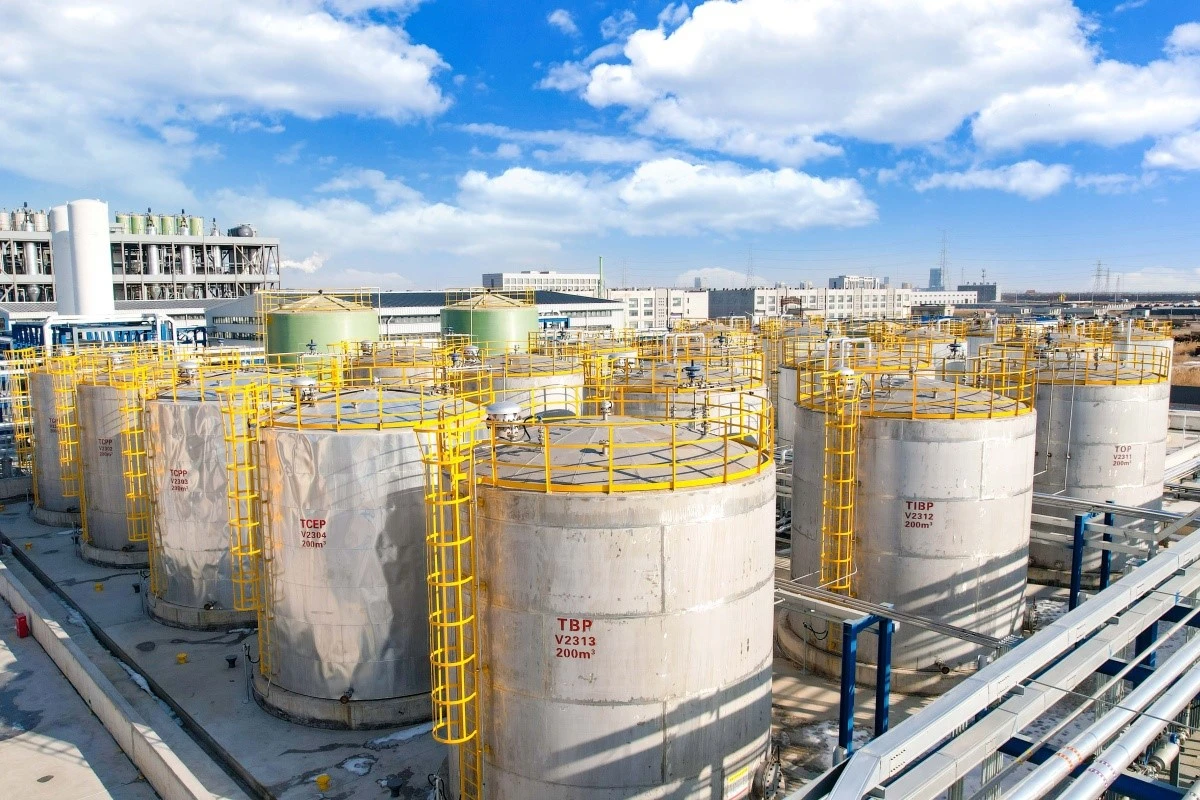
The company has a registered capital of RMB 100 million, covers an area of 115 mu (approximately 76,700 square meters), and has a total building area of 31,000 square meters, with approximately 135 employees. Our major products include 100,000 tons/year of phosphorus oxychloride (POCl₃) and 150,000 tons/year of functional phosphate ester materials.
Our products are widely used in two major fields: flame retardants and metal extractants for lithium, nickel, cobalt, and other metals. They cover a wide range of advanced material applications, including polyurethane, engineering plastics, automotive, electronics, and electrical industries, serving numerous customers in China and overseas.
Our Strengths
Established: November 2021
Registered Capital: RMB 100 million
Land Area: 115 mu (approximately 76,700 m²)
Building Area: 31,000 m²
Employees: Approximately 135
Phosphorus Oxychloride Production Capacity: 100,000 tons/year
Functional Phosphate Ester Production Capacity: 150,000 tons/year
Research Institute Investment: RMB 60 million
Research Institute Area: 8,000 m²
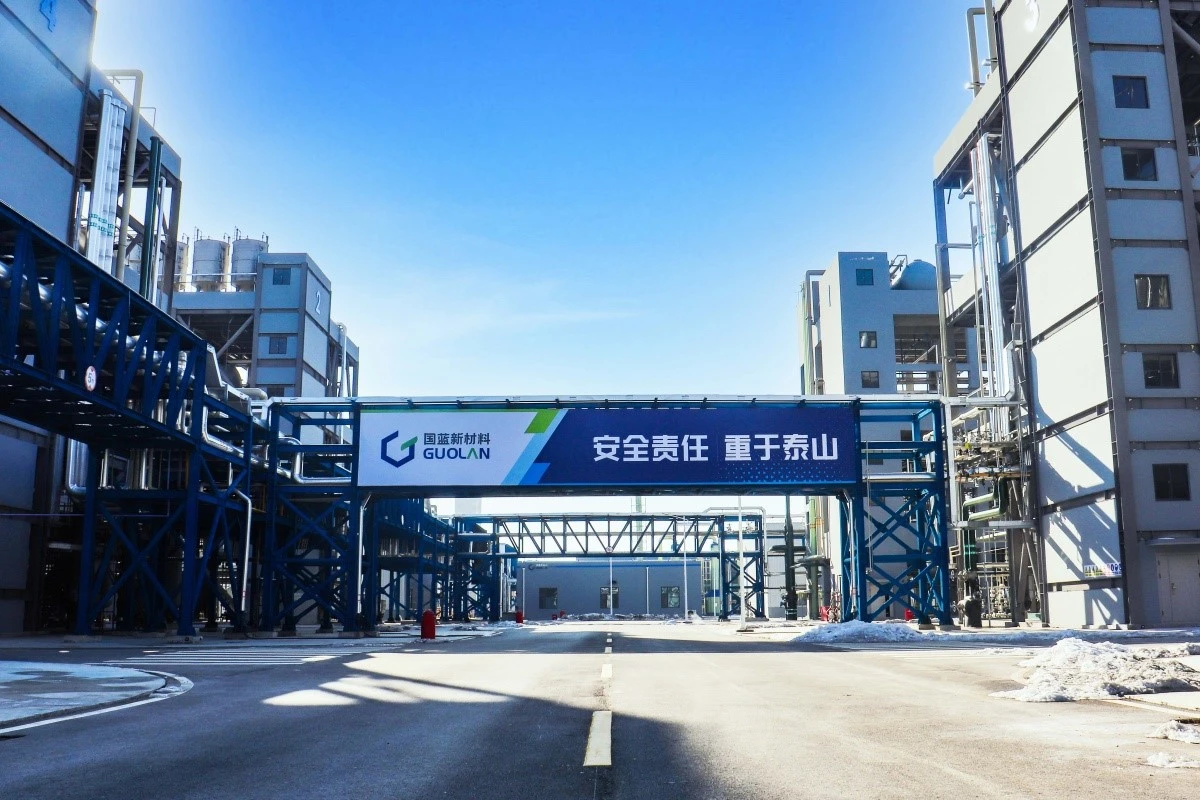
Advanced Production Equipment and Production Capacity
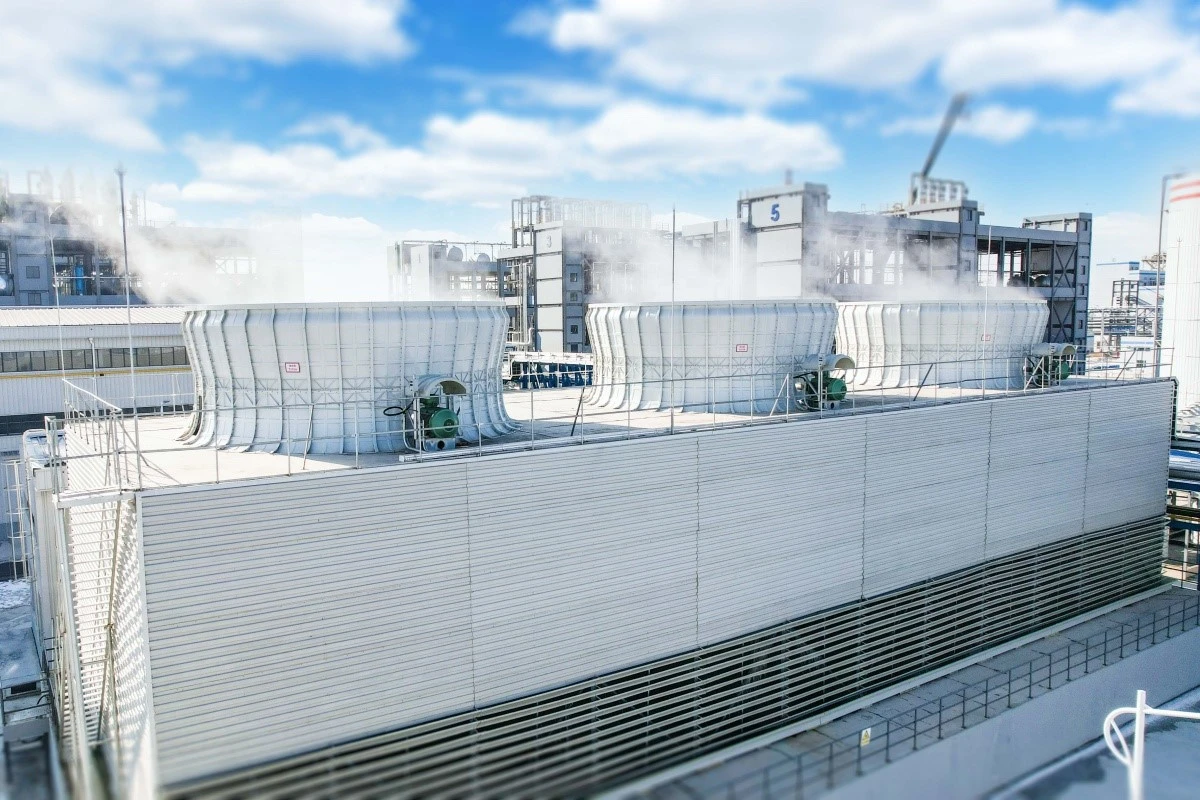
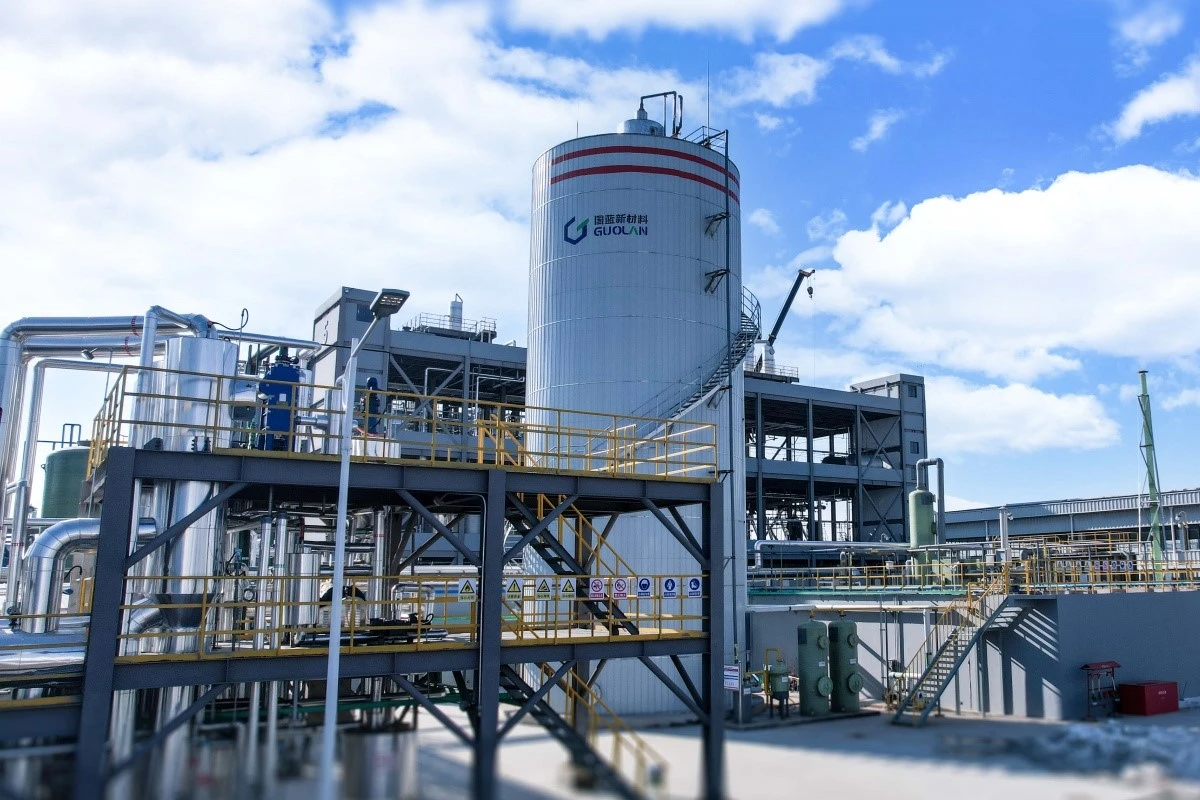
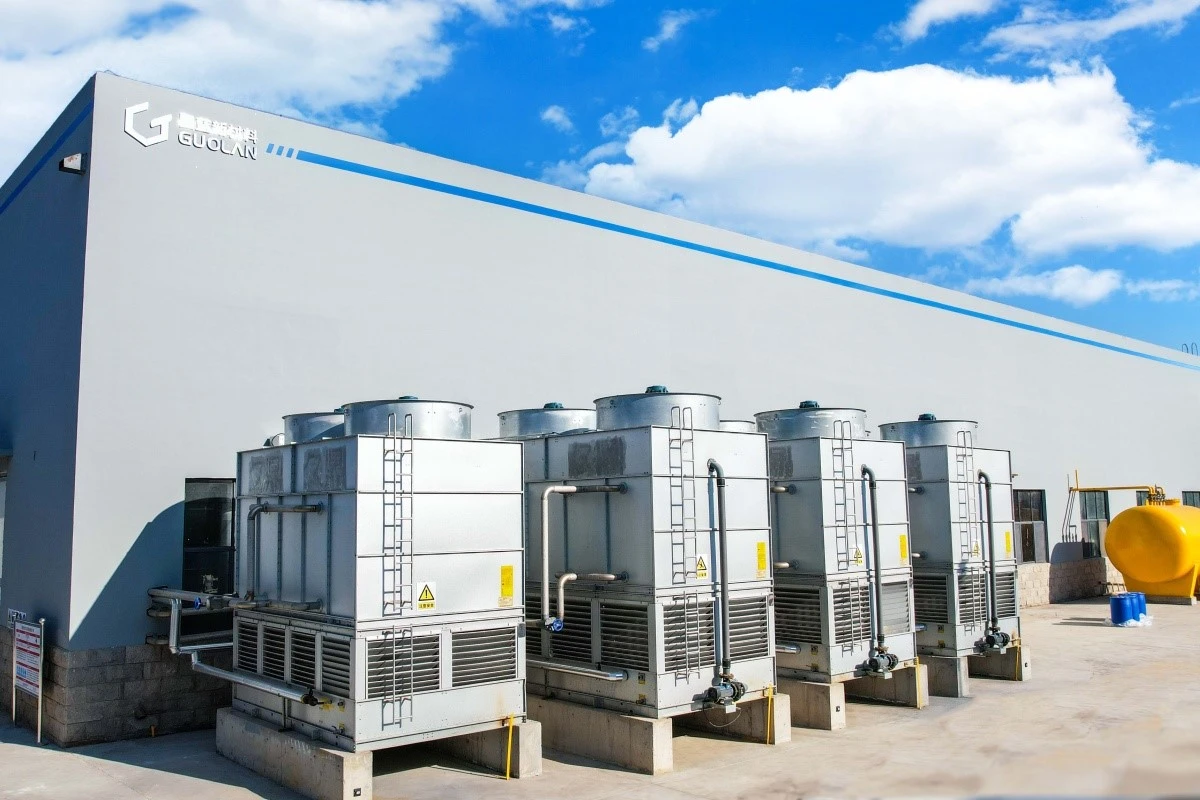
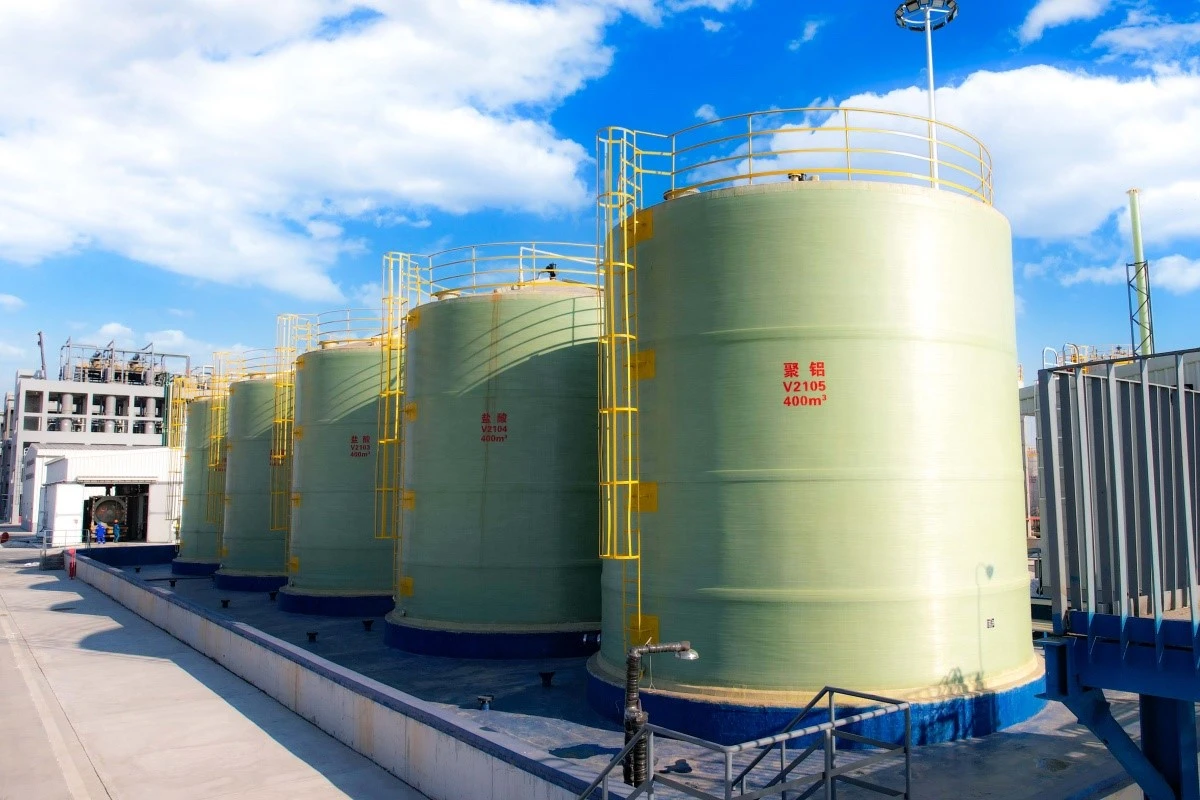
The company adopts advanced integrated equipment and intelligent production lines, enabling continuous production and integrated operation. This ensures efficient operation throughout the production process while maintaining stable product quality and sufficient production capacity.
Major Production Capacities
- Phosphorus Oxychloride (POCl₃): 100,000 tons/year
- Functional Phosphate Ester Materials: 150,000 tons/year
The company has moved beyond traditional batch reaction processes and adopted an advanced continuous production process, achieving significant improvements in both product quality stability and conversion efficiency in phosphate ester synthesis. This provides the company with distinct technological advantages in the industry.
Product Portfolio
Our products are mainly divided into three categories: flame retardants, extractants, and other products, covering a wide range of applications.
Flame Retardant Series
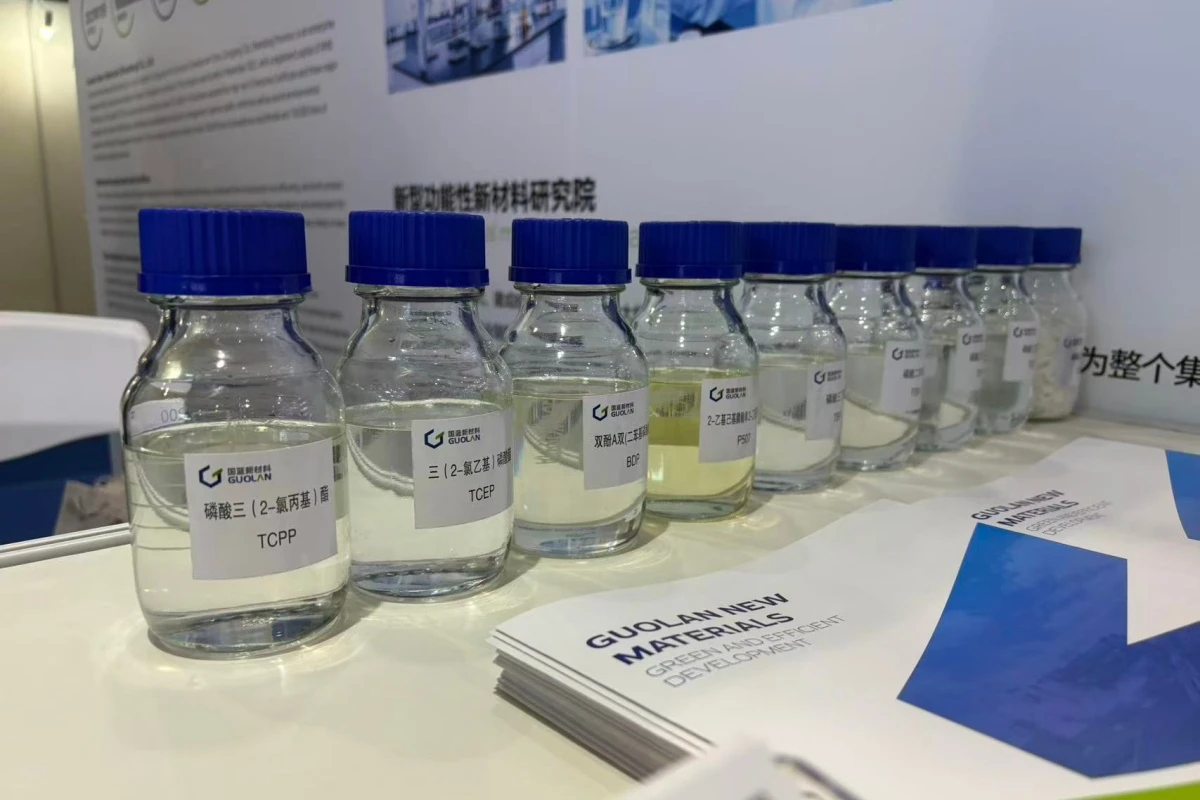
- TCPP - Tris(1-chloro-2-propyl) phosphate
A mainstream flame retardant for polyurethane foam, widely used in polyol blend systems, building spray polyurethane foam (SPF) insulation, polyurethane insulation boards, cold storage panels, automotive seat foam, and mining reinforcement materials.
- TCEP - Tris(2-chloroethyl) phosphate
A halogen-containing phosphorus-based flame retardant, used in PVC, nitrocellulose-based coatings, rubber conveyor belts, polyurethane foam, and other applications.
- TEP - Triethyl Phosphate
A halogen-free phosphorus-based flame retardant, used in rigid polyurethane foam, building insulation boards, coatings, adhesives, textiles, and other applications.
- TPP - Triphenyl Phosphate
A flame retardant for engineering plastics, used in systems such as PC/ABS.
- BDP - Bisphenol A Bis(diphenyl Phosphate)
A halogen-free flame retardant for PC/ABS, used in engineering plastics.
Extractant Series
- P204 - Di(2-ethylhexyl) Phosphate
Used as a metal extractant for nickel, cobalt, rare earth elements, and other metals.
- TBP - Tributyl Phosphate
Used as an extractant in lithium battery-related applications and rare-earth extraction.
- TOP - Trioctyl Phosphate
Used as an extractant for hydrogen peroxide.
- TIBP - Triisobutyl Phosphate
Used as an antifoaming agent and penetrant, with applications in cement and concrete, inks, coatings, oilfield additives, and other fields.
Other Products
- Phosphorus Oxychloride (POCl₃)
A fundamental raw material in the phosphorus chemical industry, used in pharmaceuticals, agrochemicals, and phosphate ester synthesis.
- PAC - Polyaluminium Chloride
A flocculant for water treatment.
- High-Hydrogen Silicone Oil
Used as a foam stabilizer and hydrophobic agent.
R&D Capabilities and Technological Innovation
The company places strong emphasis on product R&D and technological innovation. All patents and technologies are independently developed by the company.
The company has also established its own Research Institute to provide strong technical support for product development and applications.
R&D Platform
- New Functional Materials Research Institute
R&D Focus
- Research on the synthesis of green halogen-free flame retardants
- New-energy lithium battery recycling
- Research on the synthesis of non-ferrous metal extractants
- Research and development of metal-organic compounds
- Research on pharmaceutical intermediates and related industries
R&D Team
The company integrates resources from renowned universities in China and brings together a number of outstanding academic leaders and experts.
- Number of R&D Personnel: 123
- Number of Patents: 123
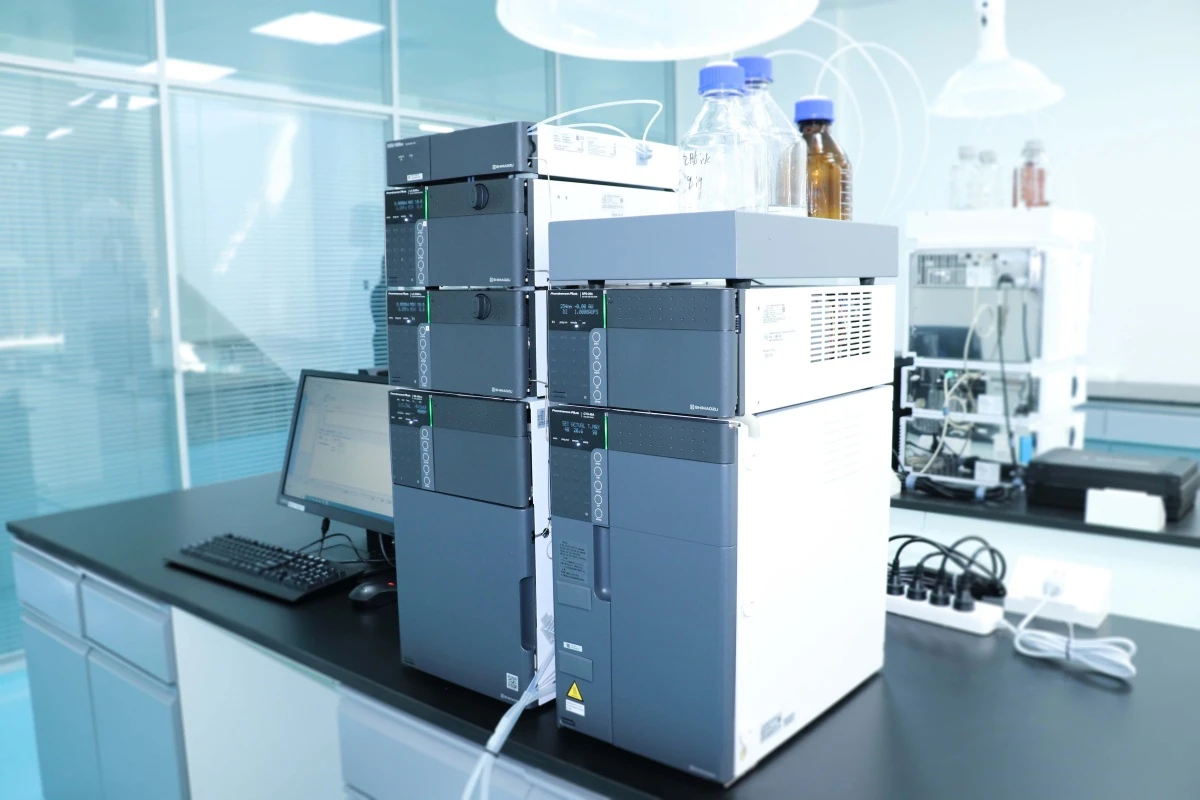
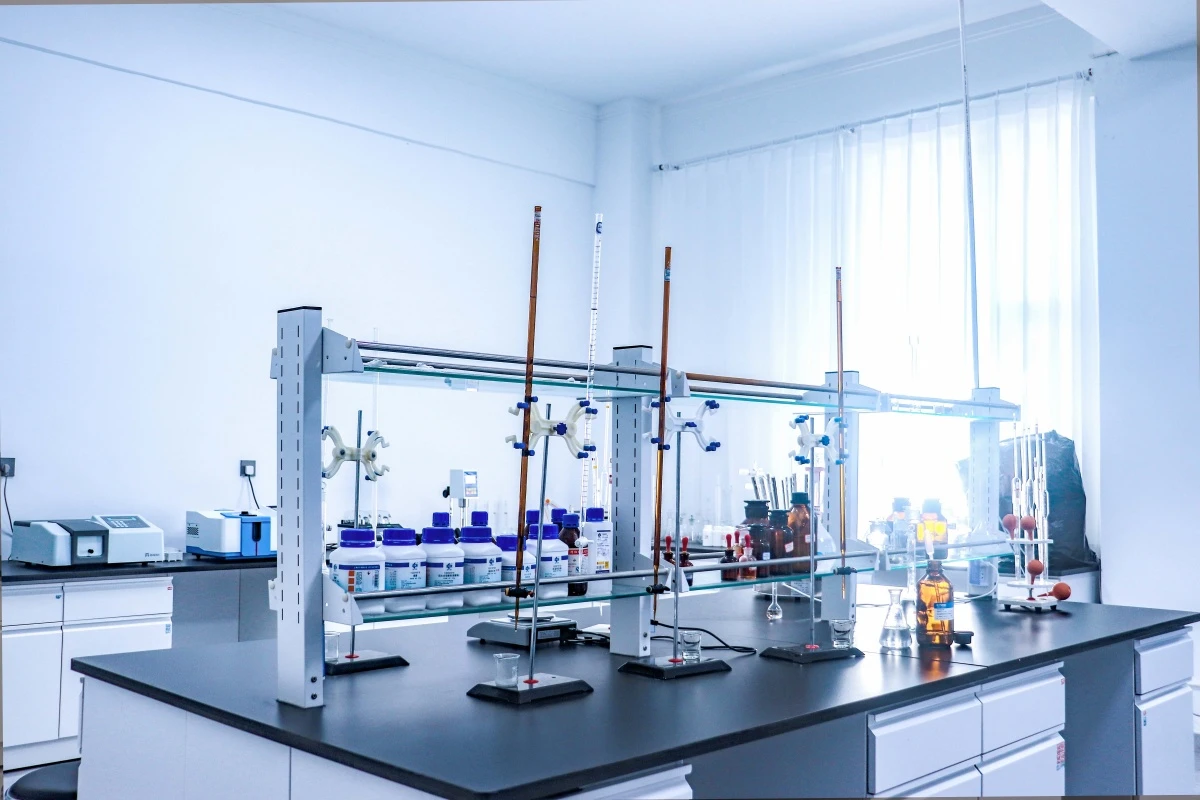
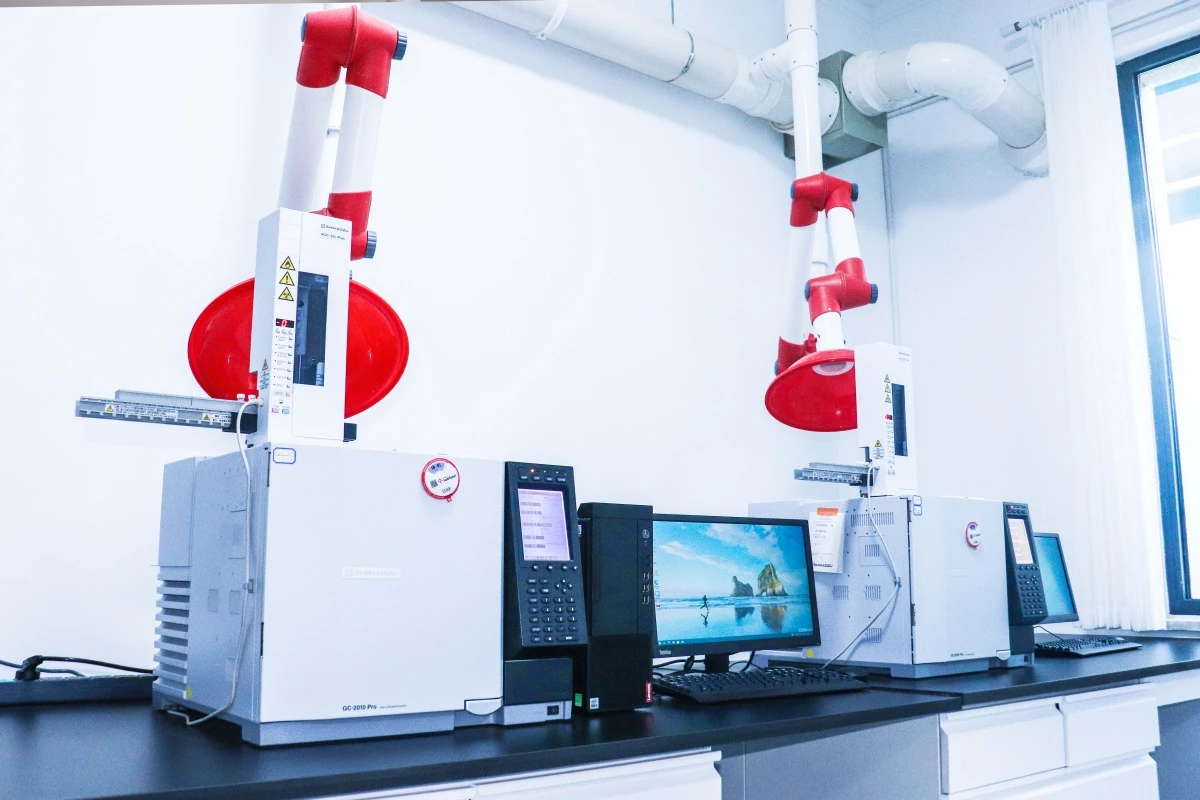
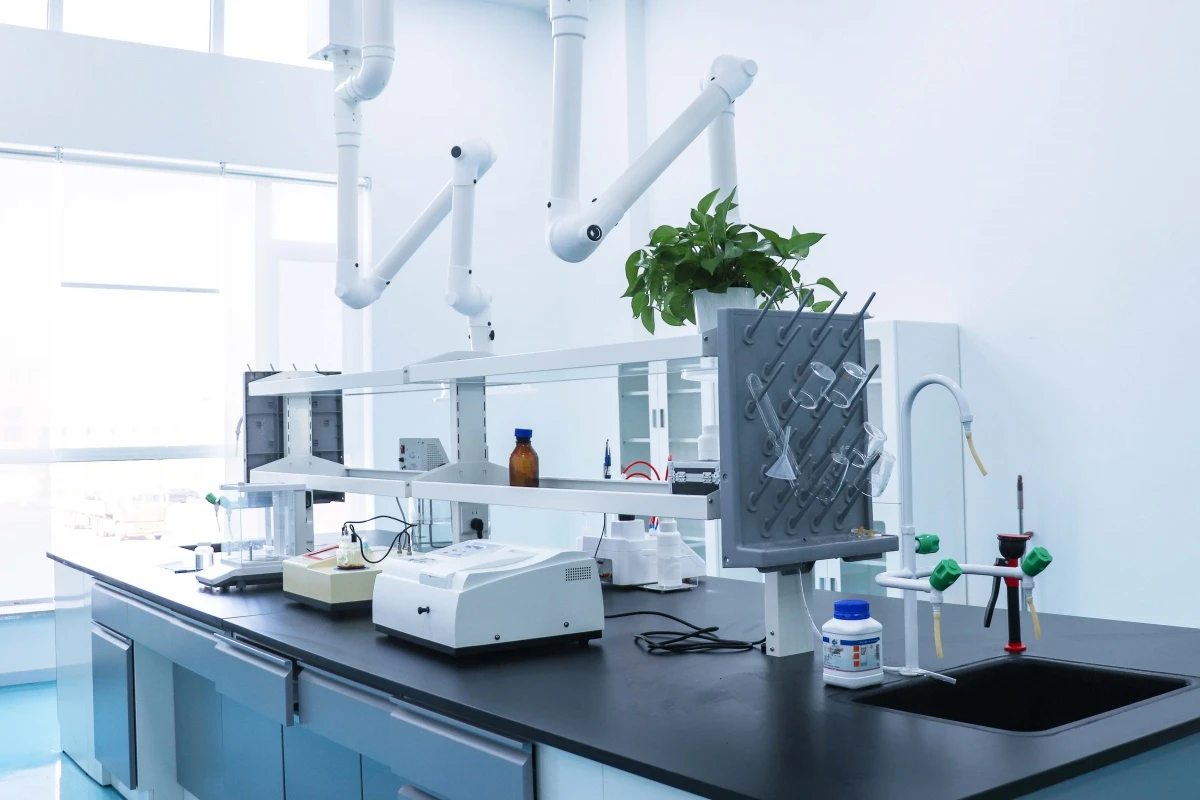
New Functional Materials Research Institute
With a total investment of RMB 60 million, the Research Institute has established an 8,000-square-meter comprehensive R&D building. It is committed to developing an advanced R&D platform for high-end new materials and chemical technologies, providing technical support for the Group's development and the chemical industry chain in Dongying.
The company integrates resources from renowned universities in China and brings together a number of outstanding academic leaders and experts. Focusing on the research and development of high-end chemical additives and advanced new materials, the company has established the New Functional Materials Research Institute.
Its research areas include:
- Research on the synthesis of green halogen-free flame retardants
- New-energy lithium battery recycling
- Research on the synthesis of non-ferrous metal extractants
- Research and development of metal-organic compounds
- Research on pharmaceutical intermediates and related industries
Objectives of the Research Institute
1. R&D of Common and Key Technologies
Overcome key technologies in high-end chemical additives and advanced new materials while strengthening collaborative innovation.
2. Commercialization of Technological Innovations
Promote the industrialization of research achievements and achieve the seamless integration of technology and industry.
3. Incubation of Innovative Enterprises
Support the growth of innovative enterprises and promote the integrated development of research, development, industrialization, and incubation.
4. Public Technical Services for the Industry
Establish a public technology service platform and promote the open sharing of resources.
5. Talent Development and Collaboration
Attract and cultivate high-level professionals, establish an industry-oriented talent development base, and promote cooperation and technical exchanges.
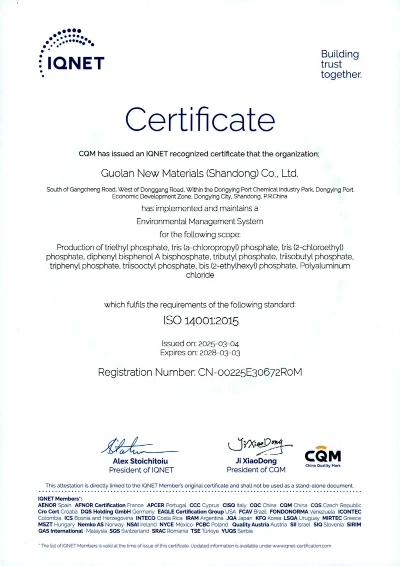
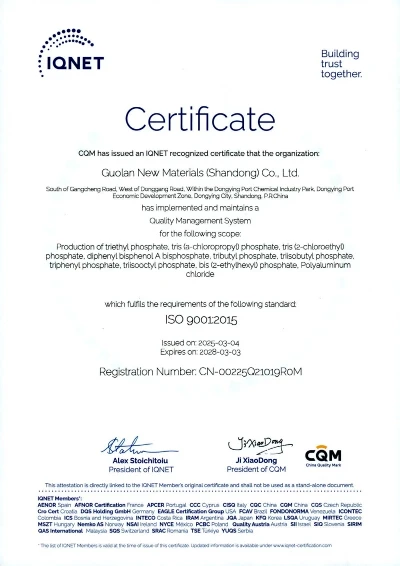
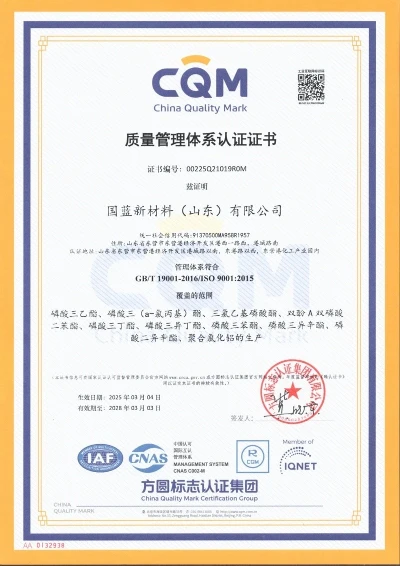
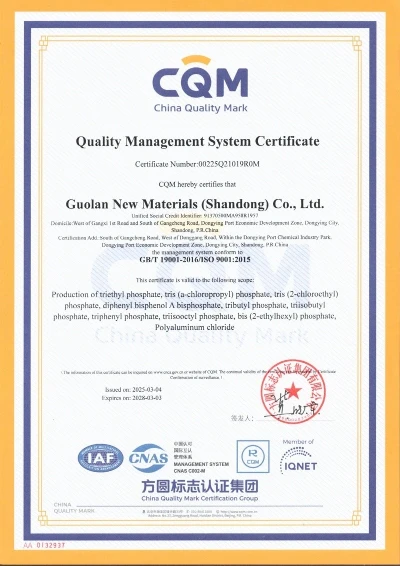
7. Quality Management System and Testing Capabilities
The company regards quality as a core priority and has established a comprehensive quality management system. From the arrival of raw materials to the shipment of finished products, quality is controlled throughout the entire production process.
Quality Management System
To be completed, e.g. ISO 9001
Product Testing Capabilities
The company is equipped with advanced testing instruments, including gas chromatographs, liquid chromatographs, moisture analyzers, and other analytical and testing equipment.
The company has comprehensive testing capabilities covering raw materials, intermediates, and finished products.
Every batch of products undergoes strict testing before shipment to ensure consistent and stable quality.
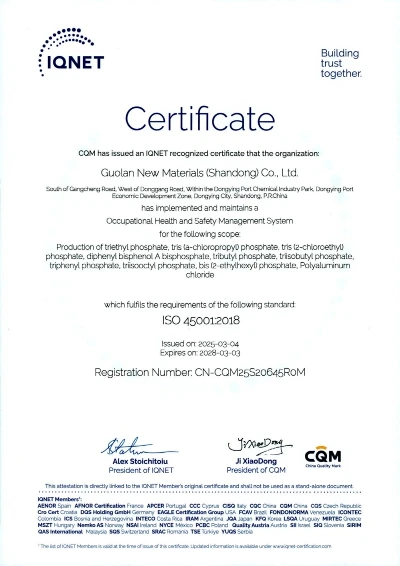
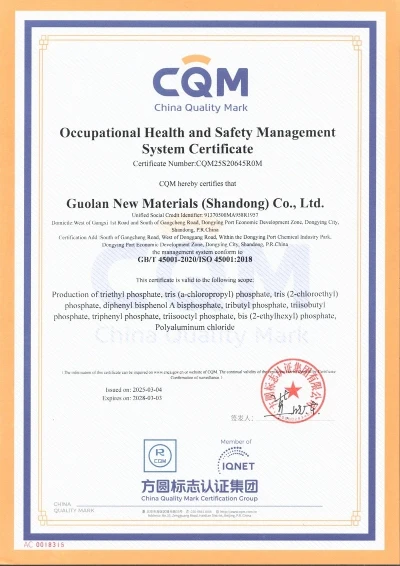
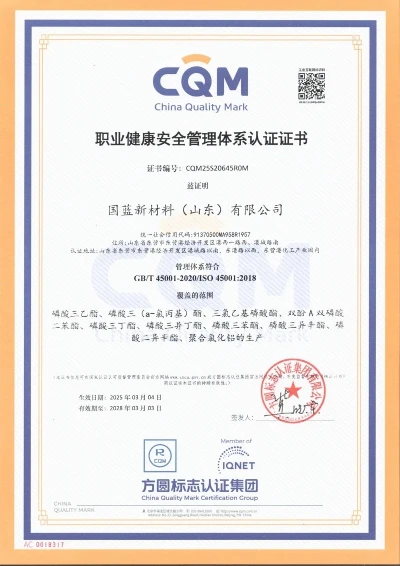
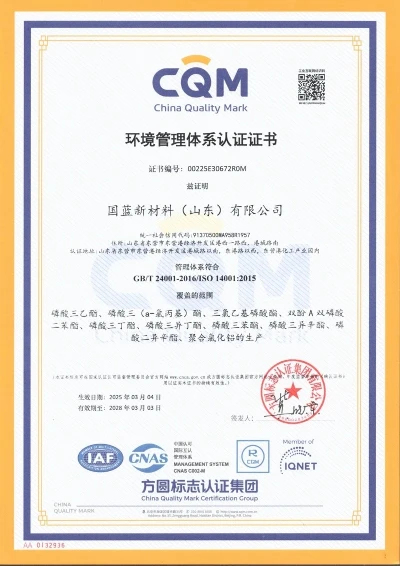
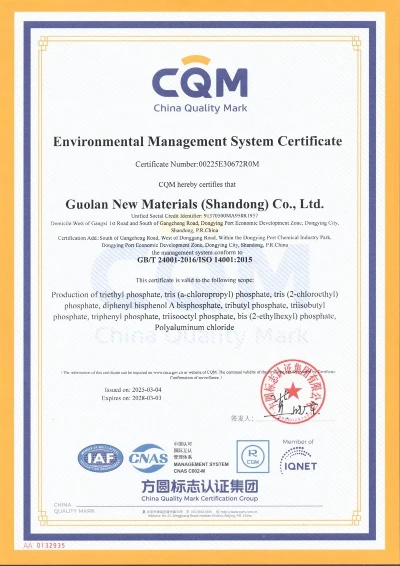
Certifications
To be completed - please list certifications obtained by the company.
Global Markets and Export Capabilities
Our products serve not only the domestic market but are also exported to multiple countries and regions.
Major Export Markets
To be completed, e.g. Australia, India, the Middle East, Southeast Asia, etc.
The company has comprehensive export operation capabilities, including customs clearance, certificates of origin, ocean freight booking, and general cargo transportation, enabling us to provide customers with one-stop service from order placement to delivery.
Packaging, Container Loading, Delivery and After-Sales Service
Packaging
Available packaging options include IBC tanks, steel drums, ISO tanks, and other packaging solutions. Customized packaging is also available according to customer requirements.
01
Container Loading
Support for full-container loads (FCL) and consolidated shipments
Professional container loading team
Photographic records throughout the loading process
02
Delivery
The company cooperates with multiple shipping lines and maintains stable sailing schedules to ensure timely delivery.
We support various international trade terms, including CIF and FOB.
03
After-Sales Service
Provision of COA, MSDS/SDS, and technical documentation
Prompt response to customer inquiries
Sample testing support
04
Why Choose Us
Factory Direct Supply
We are a source manufacturer, supplying products directly from our own factory without unnecessary intermediaries, enabling competitive pricing.
Advanced Technology
With independent R&D capabilities and continuous production technology, we are committed to maintaining stable and consistent product quality.
Strong R&D Capabilities
We have established the New Functional Materials Research Institute and continuously invest in the development of new products and technologies.
Reliable Quality
We implement comprehensive quality control throughout the entire process, from raw materials to finished products.
Stable Delivery
We maintain stable shipping schedules and timely delivery, with support for both FCL and consolidated shipments.
Long-Term Cooperation
We aim to establish long-term and stable partnerships with our customers, rather than focusing solely on one-time transactions.
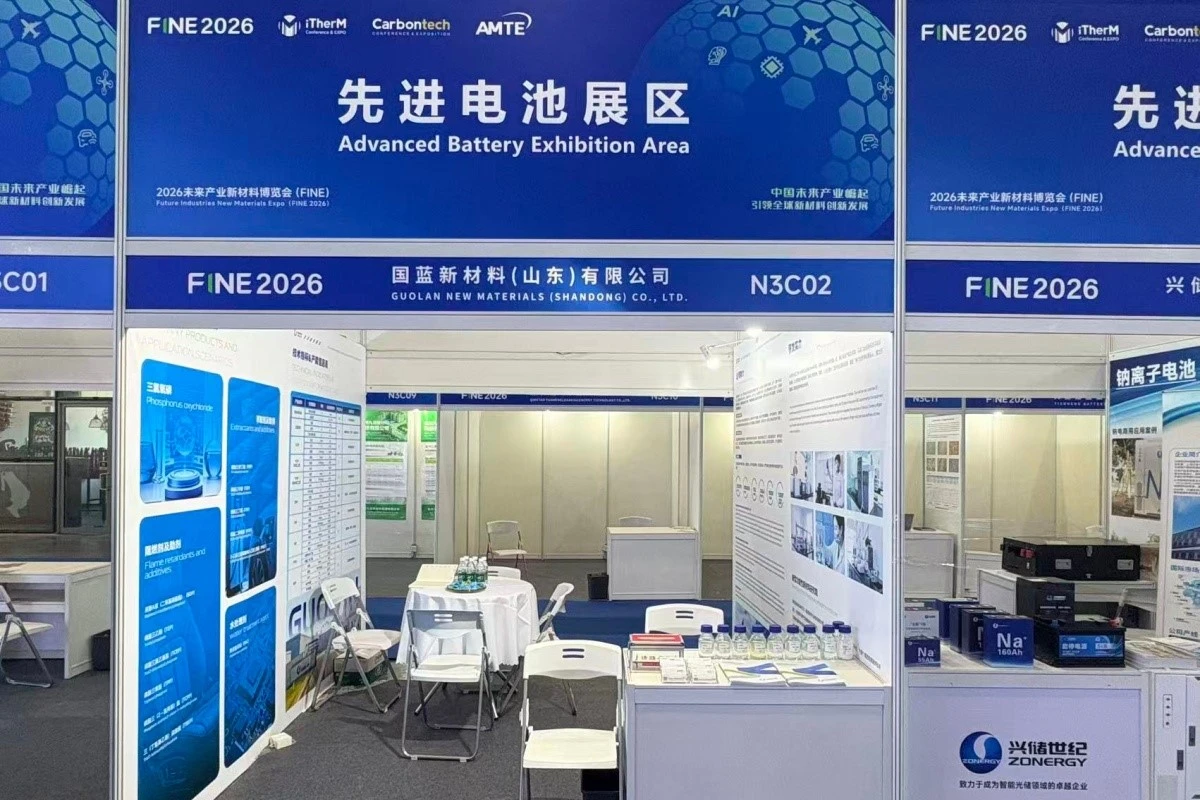
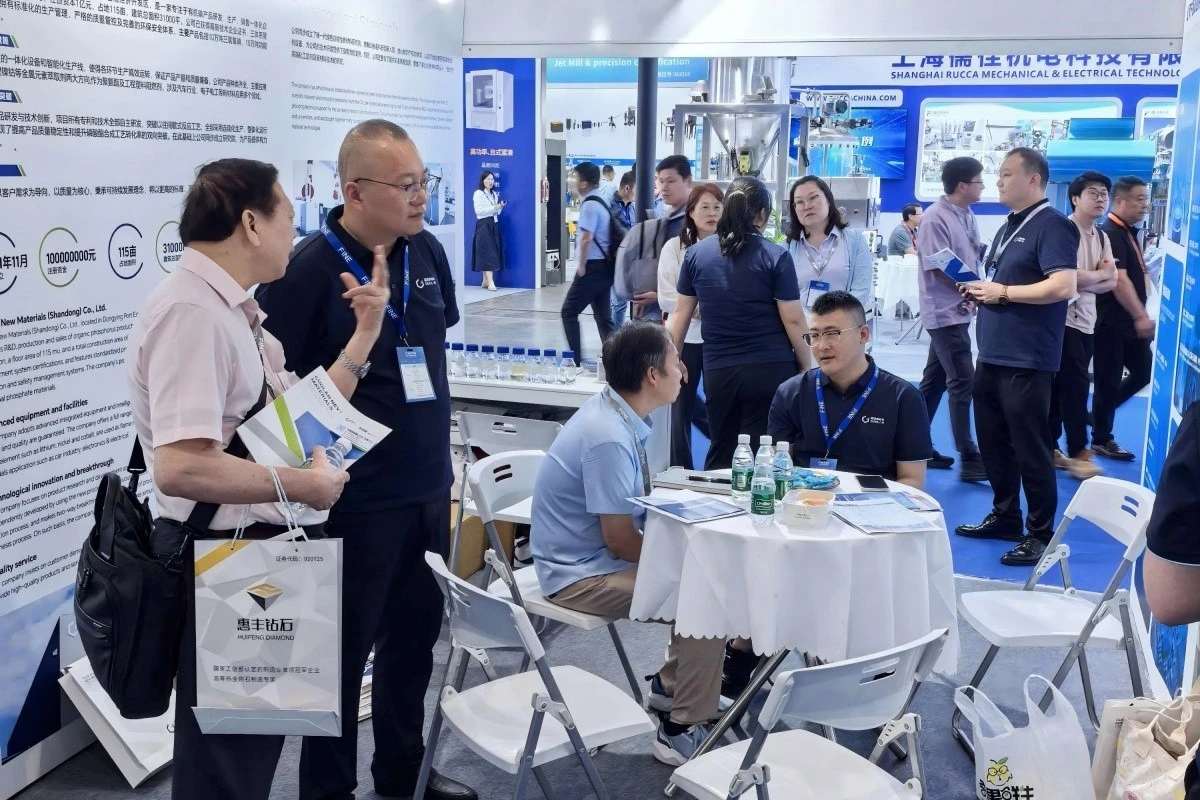
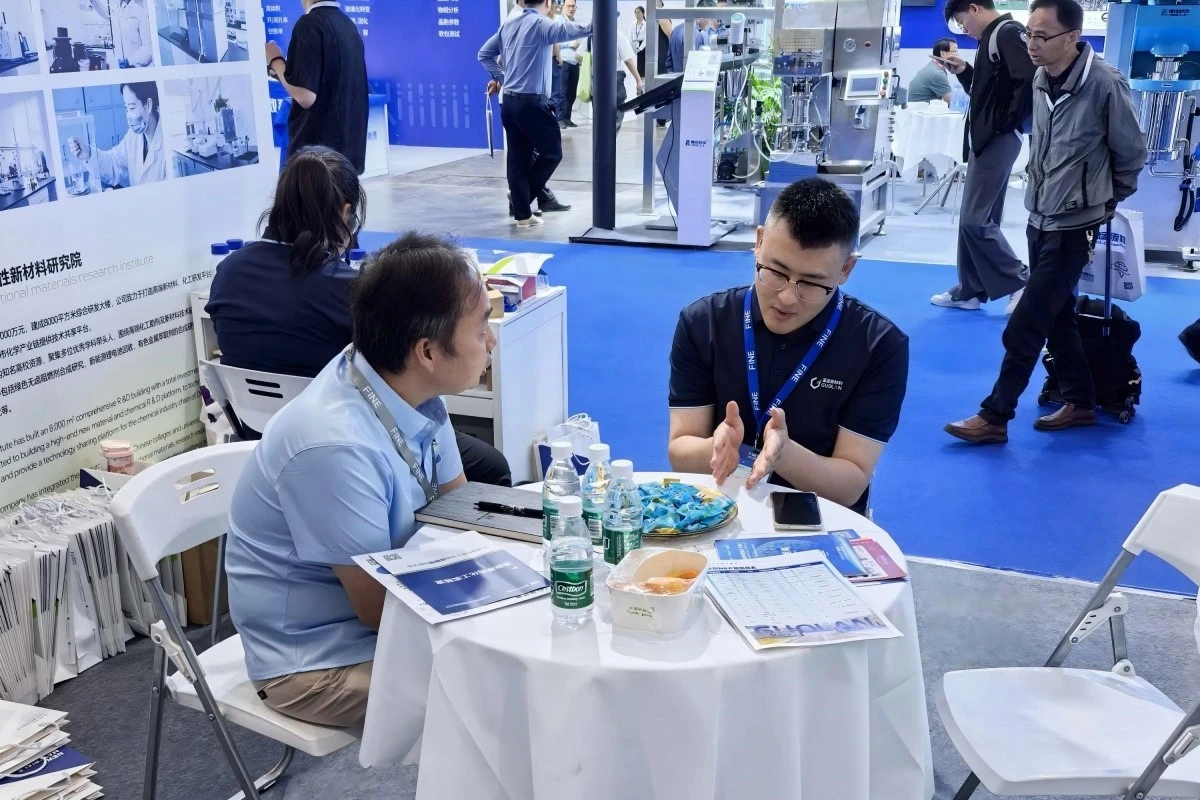
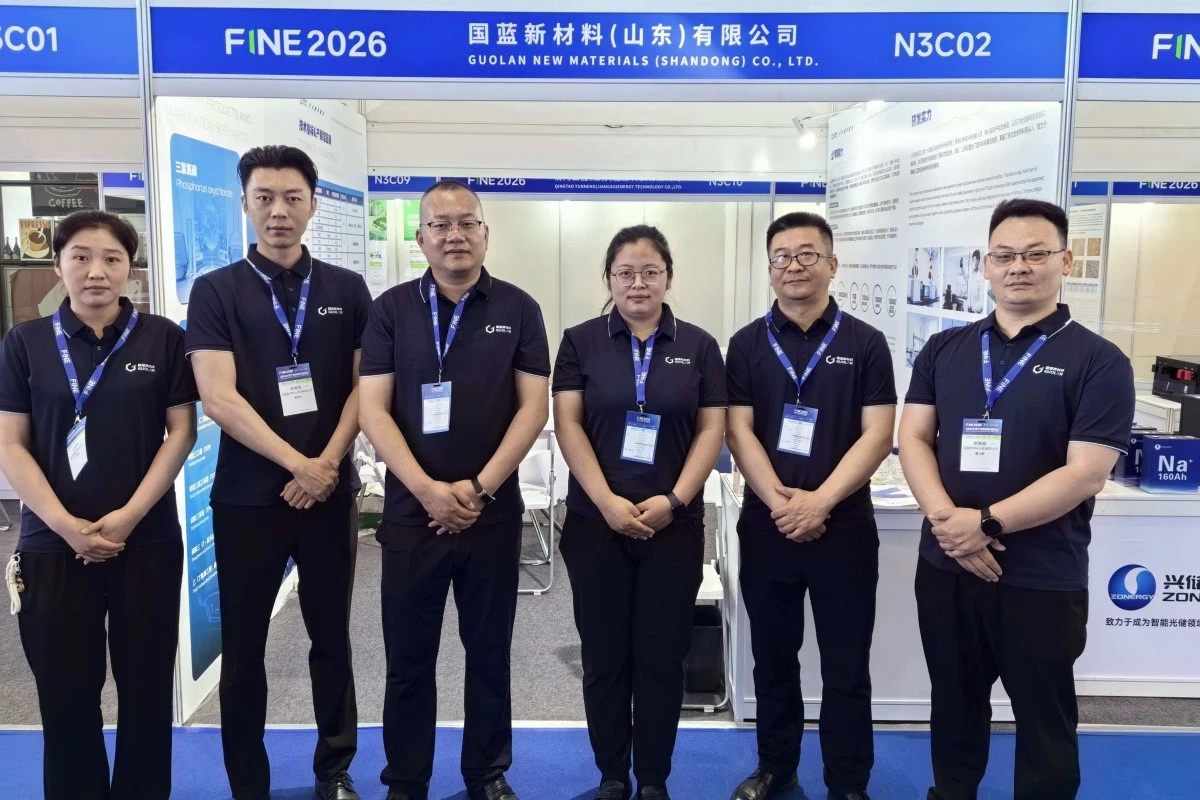
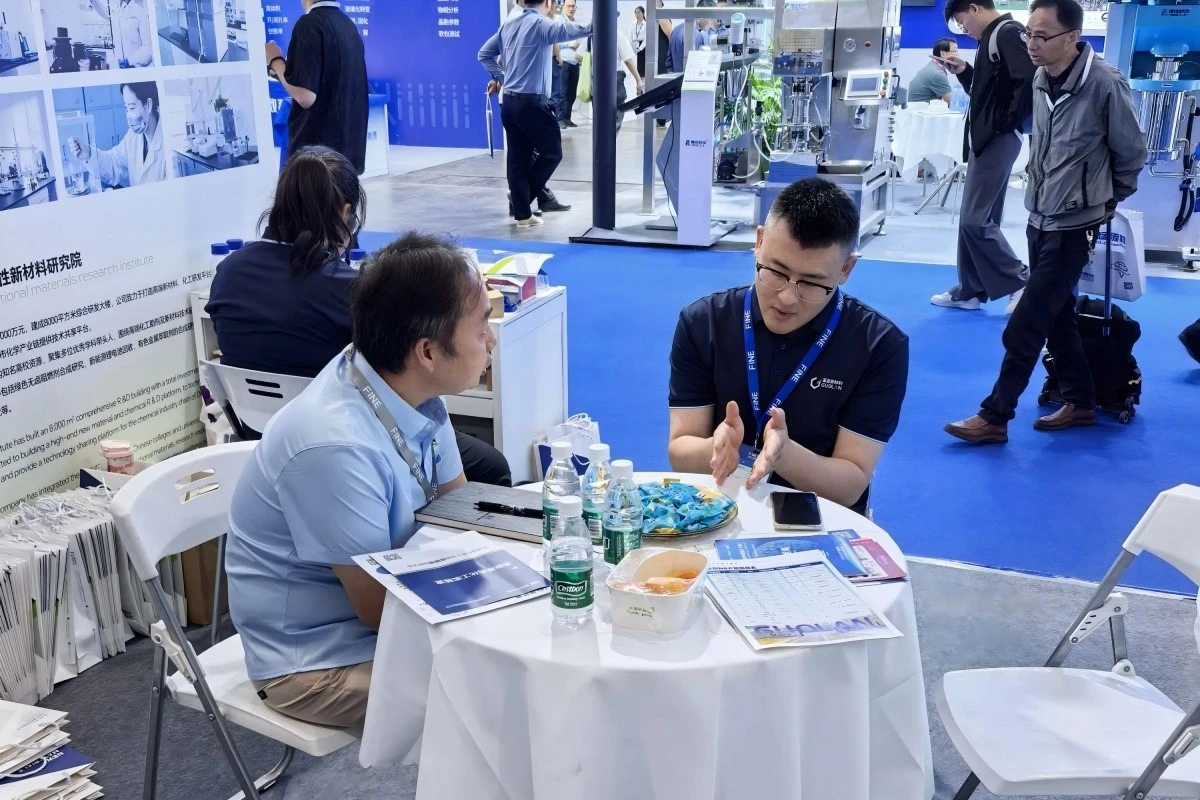
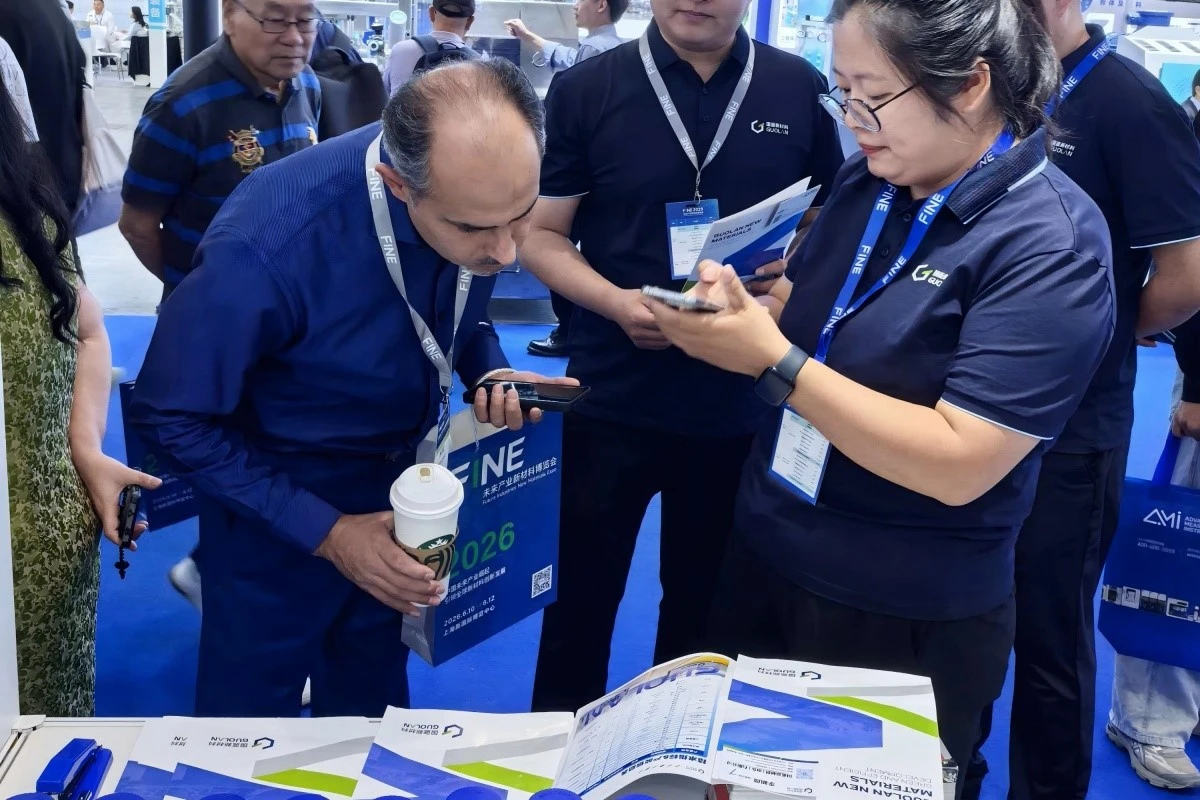
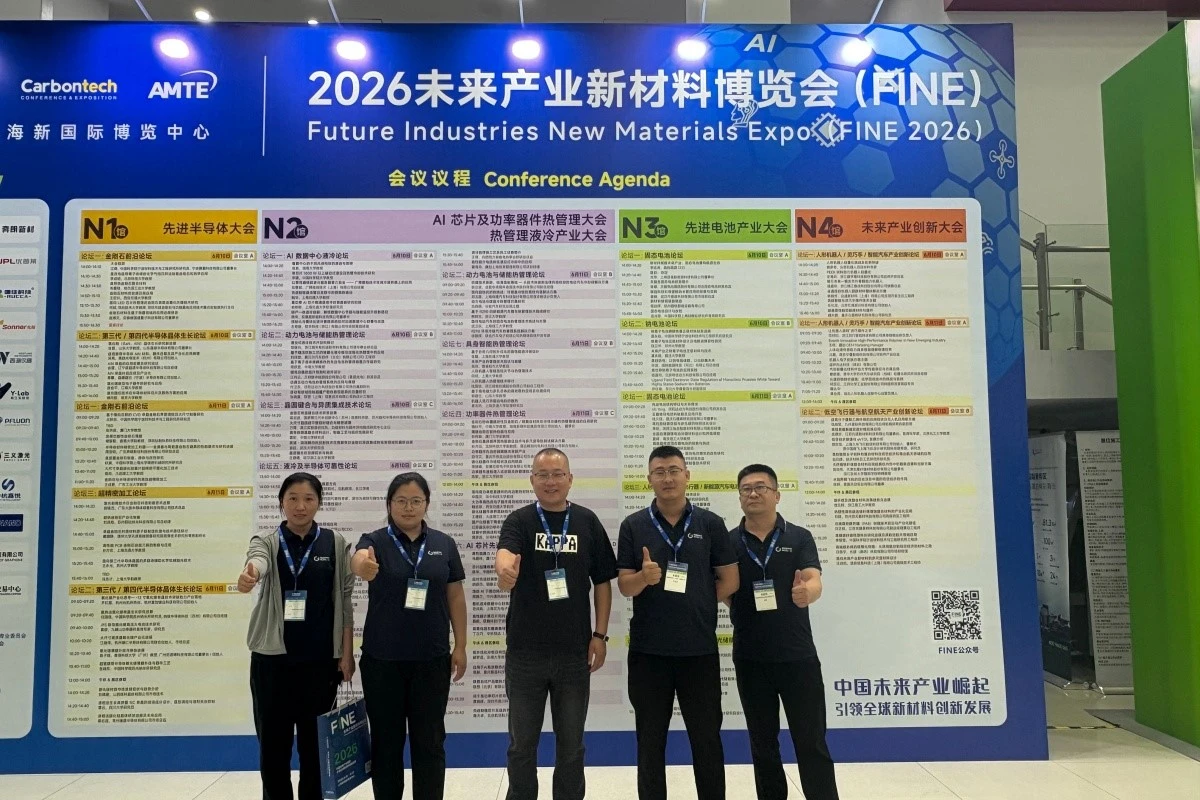
Exhibition